Top 10 Pharmaceutical Packaging Suppliers Worldwide?

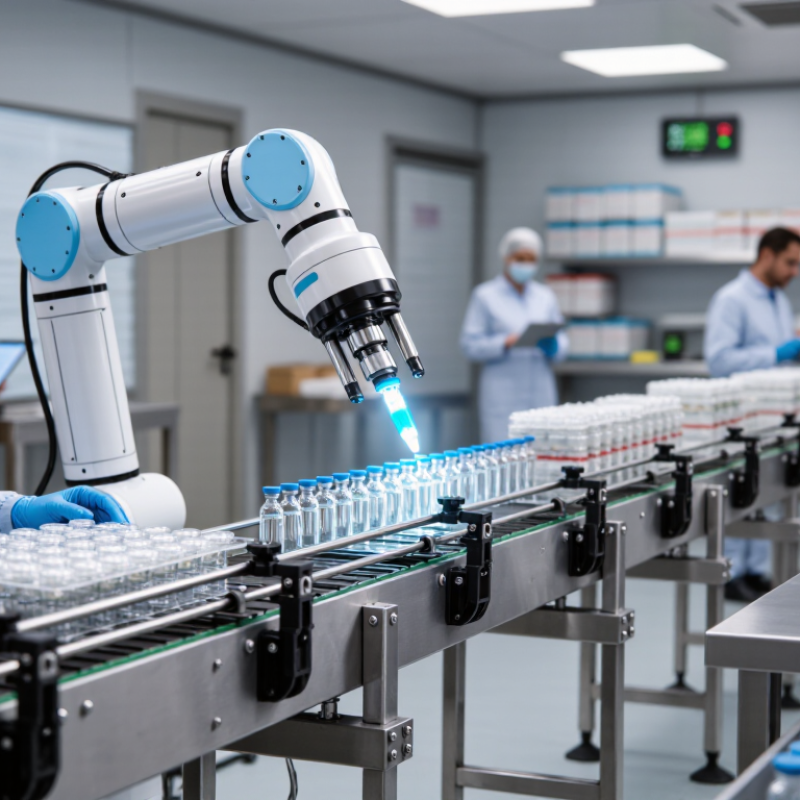
Choosing the top pharmaceutical packaging suppliers worldwide requires more than comparing revenue, factory size, or catalogue breadth. A reliable assessment must examine sterile barrier performance, child-resistant design, serialization support, material traceability, and supply continuity. These details become tangible on a production line: a blister seal is tested, a vial stopper is inspected, and every printed code must remain readable after transport.

As packaging specialist James G. Hendricks has stated, “Packaging is the last line of defense between the medicine and the environment.” This principle explains why packaging pharmaceutical systems deserve careful scrutiny. The best suppliers support formulation stability, patient safety, regulatory documentation, and practical manufacturing needs. Their value appears in controlled humidity rooms, validated sealing equipment, and documented change-control procedures.

Still, no global ranking is perfectly objective. Supplier performance can vary by region, dosage form, audit history, and customer requirements. A company strong in glass vials may not lead in flexible films or connected packaging. That limitation matters. It encourages readers to question broad claims and verify certifications, quality agreements, recall records, and delivery performance independently.

This overview identifies ten influential suppliers by considering technical capability, international reach, quality systems, innovation, and healthcare experience. It also considers less visible factors, including responsiveness during shortages and clarity in technical communication. The result is not a final verdict. It is a practical starting point for procurement teams, manufacturers, and healthcare stakeholders evaluating safer packaging pharmaceutical partnerships.
Top 10 Pharmaceutical Packaging Suppliers Worldwide?

Definition and Role of Pharmaceutical Packaging Suppliers

Pharmaceutical packaging suppliers provide the materials, components, and technical support used to protect medicines. Their work covers containers, closures, blister materials, labels, cartons, and delivery systems. Packaging is not decoration. It controls exposure to moisture, light, oxygen, contamination, and physical damage.

A reliable supplier studies the medicine before recommending a format. Tablets may need high moisture resistance, while sterile liquids require carefully controlled containers and closures. Suppliers also test seal strength, dimensional accuracy, extractables, and transport durability. In cold-chain distribution, they assess temperature protection during loading, storage, and delivery. Small details matter, such as a cap that closes evenly or a label that remains readable after condensation.

Their role also includes quality documentation and traceability. They should maintain controlled manufacturing processes, qualified equipment, trained staff, and clear change-control procedures. Batch records help customers investigate defects quickly. Packaging suppliers often support compatibility studies, stability programs, and production-scale trials. These activities require practical experience, not only catalog knowledge.

No packaging system is perfect. A material may perform well in testing but behave differently during fast production or long transport. I have seen how minor setup changes can affect seals, print clarity, or line efficiency. That is why responsible suppliers encourage risk reviews, repeat testing, and direct communication with manufacturers. They should report weaknesses honestly, even when the answer delays a shipment or requires redesign.

Key Standards for Pharmaceutical Packaging Production

When comparing the top 10 pharmaceutical packaging suppliers worldwide, production standards deserve more attention than market visibility. The World Health Organization reports that approximately one in ten medicines in low- and middle-income countries is substandard or falsified. Packaging cannot solve every quality risk, but weak seals, unclear labels, and poor traceability can increase exposure.

ISO 15378 connects pharmaceutical packaging production with good manufacturing practice. It emphasizes controlled processes, risk management, hygiene, and documented change control. For sterile products, EU GMP Annex 1 requires a contamination control strategy across production areas. Supplier audits should examine cleanroom behavior, particle monitoring, seal validation, and defect investigations. Certificates are not enough. Inspect the evidence.

Material compatibility also matters. USP chapters <661.1> and <661.2> address plastic packaging systems and extractable risks. ASTM D4169 can support distribution testing for vibration, shock, and compression. A 2024 Smithers industry study identifies regulatory compliance and sustainability as major purchasing drivers in pharmaceutical packaging. Yet lighter materials may reduce transport emissions while creating new barrier or stability concerns. That trade-off deserves testing, not assumptions. The best supplier is not always the largest. It is the one that can show repeatable results, honest deviation reporting, secure data, and practical experience with the product’s storage and transport conditions.

Top 10 Pharmaceutical Packaging Suppliers Worldwide? - Key Standards for Pharmaceutical Packaging Production

No. Standard or Regulation Primary Packaging Application Key Production Requirement Typical Compliance Evidence Global Relevance
01 ISO 15378:2017
Primary packaging materials for medicinal products
Glass, plastic, elastomeric and other primary packaging components Applies ISO 9001 quality principles together with pharmaceutical good manufacturing practices and risk-based controls. Certified quality-management system, batch records, deviation control and traceability documentation Very High
02 ISO 11607-1:2019
Packaging materials and sterile barrier systems
Sterile medical and pharmaceutical packaging materials Defines material and preformed sterile-barrier-system requirements for maintaining sterility until the point of use. Material qualification, microbial-barrier testing, seal-strength data and aging studies Very High
03 ISO 11607-2:2019
Validation of forming, sealing and assembly processes
Heat-sealed pouches, trays, blister systems and sterile assemblies Requires documented validation of forming, sealing and assembly processes, including defined operating parameters. Installation, operational and performance qualification; process capability and seal-integrity records Very High
04 EU GMP Annex 1
Manufacture of sterile medicinal products
Packaging operations used for sterile drug products Emphasizes contamination-control strategy, cleanroom qualification, personnel controls and validated aseptic processes. Environmental-monitoring results, cleanroom qualification, contamination-control strategy and media-fill records Very High
05 ISO 14644-1:2015
Classification of air cleanliness
Cleanrooms and controlled environments for packaging production Classifies air cleanliness by airborne particle concentration and supports controlled-environment design. Particle-count mapping, room qualification, airflow studies and routine environmental monitoring High
06 USP <660>
Containers—glass
Glass containers intended for pharmaceutical preparations Addresses glass classification and suitability based on hydrolytic resistance and intended pharmaceutical use. Hydrolytic-resistance testing, dimensional inspection and container qualification data High
07 USP <661.1>
Plastic materials of construction
Plastic containers and components that contact drug products Evaluates plastic materials for identity, physicochemical properties and biological safety considerations. Material identification, extractables-related testing and supplier change-control records High
08 Ph. Eur. 3.2.1
Glass containers for pharmaceutical use
Glass containers manufactured for medicinal products in European markets Sets requirements for glass types, hydrolytic resistance and container performance for pharmaceutical use. Pharmacopoeial test results, glass-type declarations and lot-release documentation High
09 21 CFR Parts 210 and 211
U.S. current good manufacturing practice
Packaging components and operations supporting drug manufacturing in the United States Requires controls for facilities, equipment, materials, production, laboratory testing, records and quality systems. Audit trails, batch documentation, quality-unit approval, complaint handling and investigation records Very High
10 ASTM D4169
Performance testing of shipping containers and systems
Transport packaging for pharmaceutical products and temperature-sensitive shipments Provides distribution-cycle testing for hazards such as vibration, shock, compression and handling. Distribution simulation, transit qualification, compression testing and documented test reports High
Evaluation note: A pharmaceutical packaging supplier should be assessed against the standards applicable to the product, packaging material, manufacturing location, market authorization and distribution conditions. Certification to a standard does not replace product-specific qualification, validation or regulatory approval.

Top 10 Pharmaceutical Packaging Suppliers Worldwide

Top 10 Pharmaceutical Packaging Suppliers Worldwide

The top 10 pharmaceutical packaging suppliers worldwide are judged by more than production volume. Reliable suppliers provide blister films, glass vials, prefilled syringes, bottles, closures, and tamper-evident systems. Their facilities should demonstrate validated processes, traceable materials, and consistent batch records. Packaging must protect medicines from moisture, oxygen, light, and contamination. Small defects matter.

In practical evaluations, I would inspect seal strength, dimensional accuracy, container closure integrity, and labeling control. A cold-chain project also needs packaging that tolerates refrigerated transport, vibration, and repeated handling. Supplier quality teams should explain extractables and leachables testing clearly. They should also support change control, stability studies, and documented corrective actions. Good communication is not optional.

A global ranking can still mislead. The largest supplier may not suit a small regional facility or a highly sensitive injectable product. I would compare audit findings, technical response times, emergency capacity, and regional manufacturing support. Site visits often reveal details that brochures hide, such as dusty storage areas or unclear material segregation. That is uncomfortable, but useful. Sustainable design also deserves scrutiny, although recyclable materials may require new equipment and process validation. The strongest suppliers combine engineering discipline with transparent evidence, rather than relying on impressive claims.

Packaging Solutions and Technologies Offered by Leading Suppliers

Top 10 Pharmaceutical Packaging Suppliers Worldwide?

Leading pharmaceutical packaging suppliers now provide more than containers. They combine barrier protection, traceability, automation, and patient-friendly design. Grand View Research estimated the global pharmaceutical packaging market at USD 108.7 billion in 2023. Its forecast points to continued growth through 2030, driven by biologics, injectable medicines, and home treatment.

The strongest suppliers typically offer blister packs, glass vials, prefilled syringes, bottles, and flexible films. Many also provide serialization, tamper evidence, vision inspection, and automated filling lines. These technologies help reduce mix-ups and reveal packaging damage before shipment. The WHO reported that about one in ten medical products in low- and middle-income countries is substandard or falsified. Packaging cannot solve that problem alone. However, authentication features and digital traceability create useful control points. Cold-chain packaging is also expanding. Smithers identifies temperature-sensitive medicines as a major driver of advanced insulated shippers and monitoring devices. A practical detail matters here: a label must remain readable after condensation, friction, and warehouse handling. I would not assume the most automated solution is always the best. Complex systems can increase training needs and maintenance risks.

Tips: Ask suppliers for validated barrier data, transport-test results, extractables studies, and line-speed evidence. Check performance with your actual product, not only a sample box. Review recyclability carefully; lighter packaging can still create difficult waste streams. Small errors remain possible, so require documented corrective actions and clear quality agreements.

Factors for Comparing Pharmaceutical Packaging Suppliers

Comparing the top 10 pharmaceutical packaging suppliers worldwide requires more than reviewing market rankings. A reliable supplier should understand product sensitivity, filling conditions, and distribution risks. I examine how clearly each supplier documents its quality system. Audit records, change-control procedures, and batch traceability matter greatly. A polished website proves little.

Material performance deserves close attention. For primary packaging, compare barrier properties, dimensional tolerance, closure integrity, and extractables data. Ask for test methods, not only attractive specifications. A practical evaluation may include temperature cycling, vibration testing, and container-closure integrity checks. Small leaks can become expensive failures. Suppliers should also explain how they manage defects and customer complaints.

Operational strength is equally important. Review production capacity, backup sites, lead times, minimum order quantities, and emergency support. Check whether technical specialists can join validation discussions. Transparent pricing should separate tooling, testing, transport, and revision costs. A low quotation can hide future expenses. Environmental performance also needs evidence, such as recycled content controls or reduced material use. However, sustainability claims may be incomplete. I would request measurable data and remain cautious about impressive wording. No supplier is perfect, and my comparison can still miss regional disruption or an unnoticed process change. Regular reassessment is therefore necessary.

Top 10 Pharmaceutical Packaging Suppliers Worldwide: Comparison Factors

The chart presents a 100-point procurement weighting model for comparing pharmaceutical packaging suppliers without using company or brand data. The criteria are aligned with common pharmaceutical packaging expectations, including GMP quality systems, regulatory compliance, container-closure integrity, supply reliability, and sustainability.

Quality and regulatory performance receive the highest weights because pharmaceutical packaging must protect product identity, strength, quality, and purity throughout its intended shelf life.